Choosing between an 80 TPH and a 120 TPH asphalt plant is not simply a matter of selecting a larger machine. It is an investment decision that directly affects project schedules, production costs, equipment utilization, and long-term profitability. While a 120 TPH asphalt mixing plant usually requires a higher initial investment, it can also produce more asphalt mixture within the same working period. However, higher rated capacity does not automatically mean higher profits.
For road construction contractors, asphalt producers, and infrastructure companies, the real question is whether the additional 40 tons per hour can generate enough revenue or operational savings to justify the purchase price difference. The answer depends on annual production demand, project duration, transportation arrangements, fuel consumption, local market conditions, and the ability to keep the plant operating efficiently.
In this guide, we compare 80 TPH and 120 TPH asphalt plants from a practical business perspective. We also explain when upgrading to 120 TPH makes financial sense, when an 80 TPH model is sufficient, and how to calculate the right capacity for your construction projects.
1. What Is The Actual Production Difference Between 80 TPH And 120 TPH?
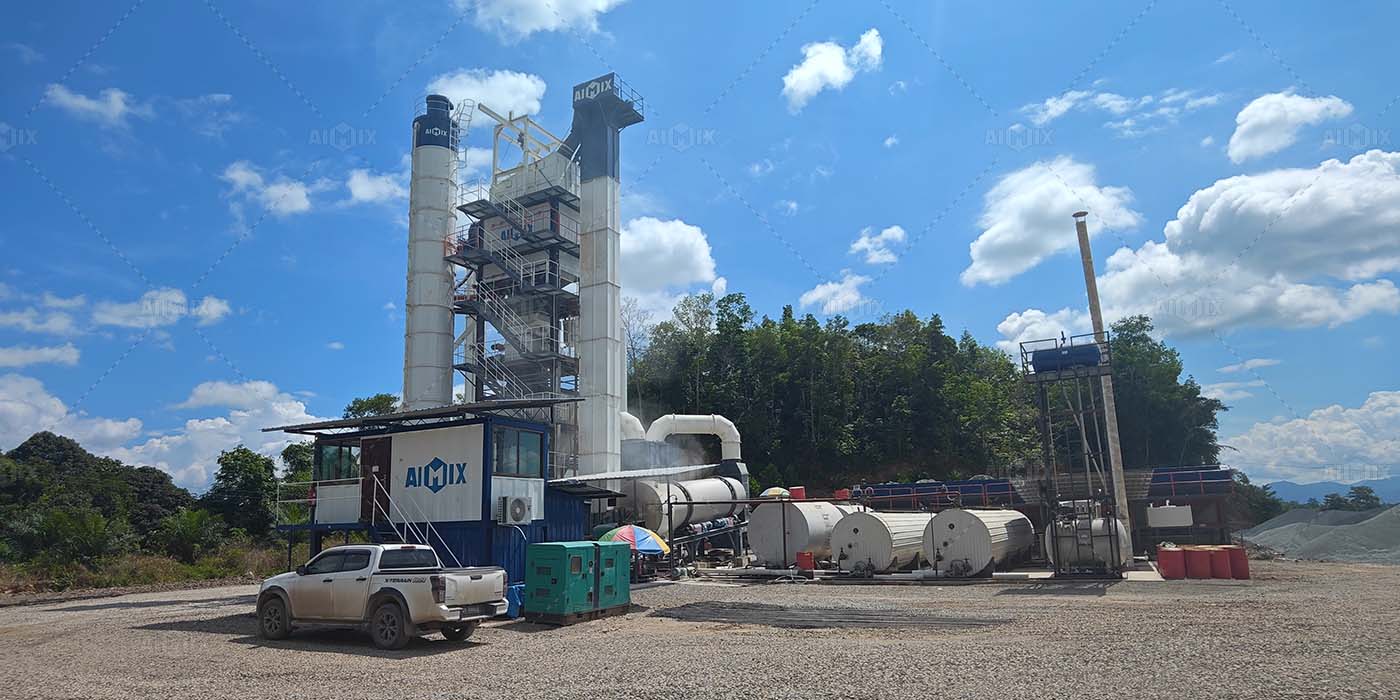
The first step is understanding how much additional asphalt mixture a 120 TPH plant can produce. The rated capacity provides a useful starting point, but actual production depends on material conditions, mix design, operating efficiency, and plant configuration. Contractors comparing different tarmac asphalt plants should therefore consider both rated output and achievable production under their working conditions.
Rated Capacity And Theoretical Production
An 80 TPH asphalt mixing plant has a rated production capacity of 80 tons per hour under specified operating conditions. A 120 TPH model increases this figure to 120 tons per hour, providing 50% more rated production capacity.
To understand the difference, consider the following theoretical production figures:
- 80 TPH asphalt plant: 640 tons during an 8-hour production shift.
- 120 TPH asphalt plant: 960 tons during an 8-hour production shift.
- Production difference: 320 additional tons per 8-hour shift.
- Daily production difference: 320 tons when both plants operate for the same 8 hours at rated capacity.
These figures represent theoretical output rather than guaranteed daily production. Actual output may be lower because of cold aggregate moisture, burner performance, material feeding interruptions, mix changes, maintenance, and truck loading delays.
Estimated Production Under Different Operating Efficiencies
In real construction operations, asphalt plants rarely maintain their maximum rated output throughout an entire shift. For preliminary planning, contractors can use an assumed production efficiency of 75% to 85%. This is an illustrative planning range, not a guaranteed industry benchmark.
- 80 TPH at 75% efficiency: Approximately 60 tons per hour, or 480 tons in an 8-hour shift.
- 80 TPH at 85% efficiency: Approximately 68 tons per hour, or 544 tons in an 8-hour shift.
- 120 TPH at 75% efficiency: Approximately 90 tons per hour, or 720 tons in an 8-hour shift.
- 120 TPH at 85% efficiency: Approximately 102 tons per hour, or 816 tons in an 8-hour shift.
Therefore, the production advantage remains significant even when both plants operate below their rated capacities. However, this advantage only creates business value when the contractor can sell, transport, and use the additional asphalt mixture.
2. When Does A 120 TPH Asphalt Plant Become More Profitable?
Higher production capacity creates opportunities, but it also increases the investment required. Therefore, contractors should evaluate whether additional production can improve project profitability rather than focusing only on the equipment’s maximum output.
Scenario 1: Large Highway Construction Projects
Large highway projects often require continuous asphalt production over extended working periods. Contractors may need to supply hundreds or thousands of tons of asphalt mixture every day to maintain paving schedules.
For example, suppose a highway contractor needs 750 tons of asphalt mixture per day.
- An 80 TPH plant operating at 75% efficiency produces approximately 60 tons per hour. It needs 12.5 production hours to supply 750 tons.
- A 120 TPH plant operating at 75% efficiency produces approximately 90 tons per hour. It needs approximately 8.3 production hours to supply the same quantity.
The larger plant can meet the daily demand within a shorter production window. This gives the contractor more flexibility to handle maintenance, material changes, unexpected interruptions, and additional orders.
Furthermore, shorter production periods may help contractors coordinate aggregate deliveries, bitumen supply, asphalt transportation, and paving operations more efficiently. For projects with strict completion deadlines, this flexibility can be commercially valuable.
Scenario 2: Multiple Road Projects Running Simultaneously
Some contractors do not operate on a single construction site. They may supply asphalt to several road sections, municipal projects, industrial parks, or private developments at the same time.
In this situation, an 80 TPH plant may struggle to satisfy overlapping delivery schedules. A 120 TPH plant provides more production capacity and helps the company respond to multiple orders without immediately investing in a second production line.
However, contractors must also consider transportation distance and delivery schedules. Producing more asphalt does not help if trucks cannot deliver the mixture to different sites quickly enough.
Scenario 3: Commercial Asphalt Production For External Customers
For companies operating asphalt plants as commercial production facilities, capacity directly influences the potential volume of sales.
A 120 TPH plant may offer a competitive advantage when local road contractors frequently purchase asphalt mixture. It allows the producer to serve more customers and handle larger orders, particularly during periods of strong construction demand.
Nevertheless, the local market must absorb the additional production. Before choosing 120 TPH, investors should evaluate the number of potential customers, annual road construction demand, competing asphalt suppliers, and average selling prices.
3. When Is An 80 TPH Asphalt Plant A Better Investment?
Although a 120 TPH plant offers higher production capacity, it is not always the most economical choice. For some contractors, an 80 TPH asphalt plant can deliver a better balance between initial investment, operating expenses, and actual production requirements.
Small And Medium-Sized Road Construction Projects
Contractors handling local roads, rural road improvements, access roads, and medium-sized municipal projects may not need 120 tons of asphalt per hour.
For example, if a project requires approximately 300 to 400 tons of asphalt mixture per day, an 80 TPH plant can often meet the demand within a reasonable production period, depending on actual operating efficiency.
Buying a larger plant for a relatively small production requirement may result in unnecessary capital expenditure and lower equipment utilization.
Seasonal Construction Demand
In some markets, asphalt production demand changes significantly throughout the year. Rainy seasons, government budget cycles, and project approval schedules can affect the number of operating days.
If a contractor only produces asphalt for several months each year, purchasing a 120 TPH plant may create additional financial pressure. The equipment still requires investment, maintenance, and site management even when production stops.
An 80 TPH model may be more suitable when annual production volume remains limited or unpredictable.
Limited Transportation And Storage Capacity
Asphalt production must remain synchronized with transportation and paving operations. If a plant produces 120 tons per hour but the available truck fleet can only transport 70 tons per hour, the additional production capacity may not translate into better project performance.
Moreover, asphalt mixture requires proper temperature control during transportation and placement. Long waiting periods can reduce mixture quality and create construction problems.
Therefore, contractors should evaluate truck availability, haul distance, paving equipment capacity, and temporary storage arrangements before upgrading to a larger plant.
4. 80 TPH Vs. 120 TPH Asphalt Plant: Which Costs More To Operate?
The initial purchase price is only one part of the investment. Contractors should also compare fuel consumption, electricity, maintenance, labor, spare parts, and production costs per ton. Understanding the complete asphalt concrete plant cost helps buyers avoid making decisions based only on the equipment purchase price.
Initial Equipment Investment
A 120 TPH asphalt plant generally requires a higher initial investment than an 80 TPH model. Its larger production capacity may involve higher-capacity drying, screening, mixing, aggregate feeding, and dust collection systems.
However, the actual price difference depends on the plant type, configuration, automation level, environmental protection equipment, storage capacity, and customization requirements.
For example, an 80 TPH batch mix asphalt plant and a 120 TPH batch mix plant may have different equipment specifications and auxiliary configurations. Buyers should compare complete quotations rather than comparing only the headline equipment prices.
Fuel Consumption And Energy Costs
The drying drum and burner system account for a major part of an asphalt plant’s energy consumption. A larger plant may consume more fuel per hour because it processes more aggregate. However, hourly fuel consumption alone does not determine which plant has the lower production cost.
Contractors should compare fuel consumption per ton of finished asphalt mixture under similar operating conditions.
For example, consider two hypothetical production configurations:
- 80 TPH plant: 600 liters of fuel consumed during an 8-hour shift, producing 480 tons of asphalt mixture.
- 120 TPH plant: 850 liters of fuel consumed during an 8-hour shift, producing 720 tons of asphalt mixture.
Based on these illustrative figures, the 80 TPH plant consumes approximately 1.25 liters per ton, while the 120 TPH plant consumes approximately 1.18 liters per ton.
Although the larger plant consumes more fuel per hour, its fuel consumption per ton is slightly lower in this example. Actual results depend on aggregate moisture, burner efficiency, production stability, mix temperature, and operating conditions. Buyers should request verified fuel consumption data from suppliers using comparable materials and production conditions.
Labor And Maintenance Expenses
A 120 TPH plant does not necessarily require 50% more operators than an 80 TPH plant. Both systems may use similar control room arrangements and automation processes.
However, the larger production line may require more attention to aggregate feeding, truck coordination, material handling, and routine maintenance. It may also involve higher costs for certain wear parts and replacement components.
For a fair comparison, contractors should calculate total annual operating expenses rather than assuming that a larger plant always has proportionally higher costs.
5. How To Calculate Whether The Additional Investment Is Worth It
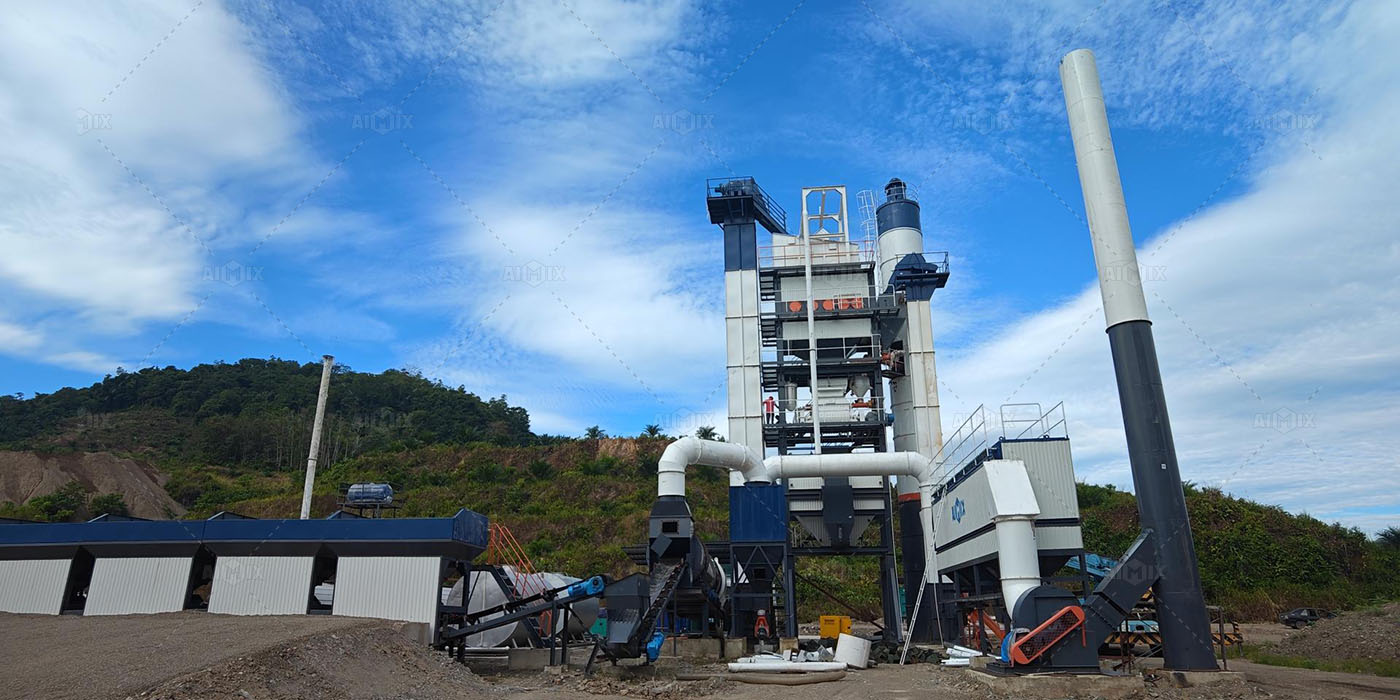
The most useful way to compare the two models is to estimate how much additional profit the 120 TPH plant can generate over the 80 TPH alternative.
Step 1: Calculate The Additional Initial Investment
First, obtain complete quotations for both models. Include equipment, transportation, installation, foundations, electrical systems, environmental equipment, storage silos, and other necessary auxiliary facilities.
Additional Investment = Total 120 TPH Project Cost – Total 80 TPH Project Cost
This approach avoids comparing an 80 TPH basic configuration with a 120 TPH package that includes additional equipment.
Step 2: Estimate Additional Annual Production
Calculate how many tons the 120 TPH plant can realistically produce beyond the 80 TPH model.
Additional Annual Production = (Actual 120 TPH Output – Actual 80 TPH Output) × Annual Operating Hours
For example, assume both plants operate for 1,000 hours per year and maintain the same 75% production efficiency.
- 80 TPH annual output: 80 × 75% × 1,000 = 60,000 tons.
- 120 TPH annual output: 120 × 75% × 1,000 = 90,000 tons.
- Additional annual production: 30,000 tons.
This calculation assumes sufficient aggregate, bitumen, labor, transportation, customer demand, and operating time. If the market cannot absorb the additional 30,000 tons, the larger capacity may remain underutilized.
Step 3: Calculate Additional Annual Contribution
Additional production does not equal additional profit. Contractors must subtract the variable costs associated with producing and delivering each additional ton.
Additional Annual Contribution = Additional Annual Sales Volume × Net Contribution Per Ton
Net contribution per ton should account for the selling price minus relevant variable costs, such as aggregate, bitumen, fuel, electricity, labor directly linked to production, and transportation where applicable.
For illustration, assume the additional 30,000 tons generate a net contribution of $5 per ton after variable costs.
- Additional annual production: 30,000 tons.
- Net contribution per ton: $5.
- Additional annual contribution: $150,000.
This figure is not a guaranteed profit forecast. Contractors must also account for additional fixed costs, financing expenses, taxes, depreciation, and any differences in maintenance requirements.
Step 4: Estimate The Additional Investment Payback Period
Once you know the additional investment and estimated annual contribution, you can calculate a simple payback period.
Simple Payback Period = Additional Investment ÷ Additional Annual Net Cash Flow
For example, assume the complete 120 TPH configuration costs $100,000 more than the comparable 80 TPH configuration. If the larger plant generates an additional $125,000 in annual net cash flow, the simple payback period is approximately 0.8 years.
However, this example uses hypothetical figures. A real investment analysis should include financing, taxes, working capital, equipment depreciation, future maintenance, and changes in market demand.
6. What Other Factors Should You Consider Before Upgrading To 120 TPH?
Even when the financial calculation looks attractive, production capacity alone should not determine the final purchase decision. Several operational factors can influence whether the larger plant performs as expected.
Aggregate Moisture And Local Climate
Wet aggregate increases the energy required for drying and can reduce actual production capacity. This issue is especially important in tropical regions and areas with frequent rainfall.
For projects in Indonesia, Malaysia, and other Southeast Asian markets, buyers should evaluate aggregate moisture, covered storage arrangements, drainage, and burner capacity. A plant that performs well with dry aggregate may achieve a different output under wet operating conditions.
Asphalt Transportation And Paving Capacity
The asphalt plant should match the capacity of the entire construction operation, not just the production target.
For example, if the paving crew can place only 70 tons per hour, operating a 120 TPH plant continuously may create unnecessary stockpiling or truck waiting time.
Before purchasing, calculate the relationship between:
- Asphalt plant production capacity in tons per hour.
- Truck payload and the number of available transport vehicles.
- Average transportation distance and round-trip time.
- Asphalt paver placement capacity.
- Daily paving hours and project completion targets.
Matching these capacities helps prevent bottlenecks and reduces the risk of producing more asphalt than the project can use.
Batch Mix Or Drum Mix Configuration
Production capacity is not the only difference between asphalt plant configurations. Contractors should also consider the type of asphalt mixture they produce and the flexibility their projects require.
A batch mix asphalt plant produces asphalt in separate batches. It allows operators to adjust mix designs and manage different production requirements. This configuration can suit contractors handling multiple road projects and asphalt specifications.
A drum mix plant for sale may be a suitable option for projects that require relatively consistent mix designs and continuous production. Its drying and mixing processes take place continuously, which can simplify production for certain road construction operations.
Therefore, choosing between an 80 TPH and 120 TPH plant should also involve evaluating production methods, mix requirements, environmental standards, and operating preferences.
Future Business Growth
Equipment purchases often remain in operation for many years. Consequently, contractors should consider not only their current projects but also their expected workload over the next three to five years.
If a company plans to expand into highway construction, commercial asphalt supply, industrial access roads, or larger government projects, a 120 TPH plant may provide useful production capacity for future contracts.
On the other hand, if future demand remains uncertain, an 80 TPH plant may reduce financial exposure while leaving more capital available for trucks, pavers, aggregate stockpiles, and other construction equipment.
7. Which Asphalt Plant Capacity Should You Choose?
After comparing production output, investment costs, and operating requirements, the right choice becomes clearer when you match the plant capacity with your actual business model.
Choose An 80 TPH Asphalt Plant If:
- Your daily asphalt demand generally remains below 500 tons.
- You mainly handle small and medium-sized road construction projects.
- Your annual operating hours are limited or seasonal.
- Your available truck fleet and paving equipment cannot support higher production.
- You want to control initial investment and reduce financial risk.
- Your local asphalt market does not have enough demand to support 120 TPH production.
Choose A 120 TPH Asphalt Plant If:
- Your daily asphalt demand regularly reaches approximately 700 to 900 tons or more, depending on actual operating efficiency.
- You undertake large highway, airport, industrial road, or infrastructure projects.
- You supply asphalt mixture to multiple customers or construction sites.
- Your company has sufficient trucks, aggregate supply, bitumen storage, and paving capacity.
- You expect consistent annual production demand and high equipment utilization.
- The additional production can generate enough contribution to recover the higher investment within your target period.
These production ranges are planning examples rather than strict selection rules. The actual decision should reflect working hours, project schedules, local material conditions, and the plant’s guaranteed performance.
8. Why Is A Customized Asphalt Plant Configuration Important?
Even when two contractors select the same rated capacity, their ideal asphalt plant configurations may differ significantly. A highway contractor working on several projects may require different equipment from a commercial asphalt producer supplying one fixed market.
When evaluating an asphalt mix plant manufacturer, buyers should look beyond the advertised capacity. Equipment specifications, manufacturing quality, installation guidance, spare parts availability, and technical support all influence long-term operating performance.
Evaluate The Complete Production System
Before finalizing a quotation, consider the following equipment and project requirements:
- Aggregate cold feed system: Match the number and capacity of cold aggregate bins with the required mix proportions and feeding volume.
- Drying drum and burner: Select suitable drying capacity based on aggregate moisture, fuel availability, and production targets.
- Dust collection system: Configure the dust removal equipment according to environmental requirements and local regulations.
- Hot aggregate screening and mixing: Ensure the screening and mixing systems support the required production capacity and mix specifications.
- Bitumen storage and heating: Provide sufficient storage and heating capacity to maintain continuous production.
- Finished asphalt storage: Evaluate whether storage silos can support truck loading schedules and temporary delivery interruptions.
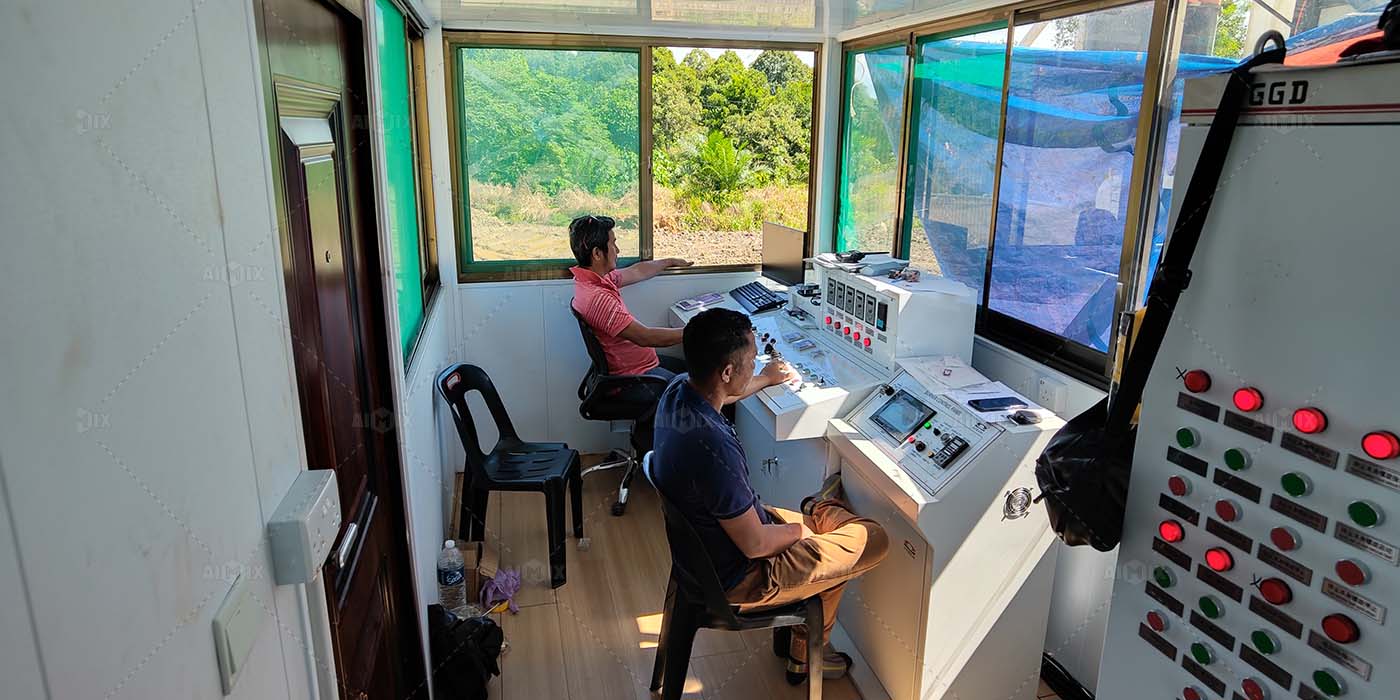
- Control system: Consider automation, production monitoring, operating convenience, and maintenance requirements.
In addition, installation conditions, foundation design, electrical supply, spare parts availability, and after-sales technical support should form part of the investment evaluation.
9. Frequently Asked Questions About 80 TPH And 120 TPH Asphalt Plants
Is A 120 TPH Asphalt Plant 50% More Expensive Than An 80 TPH Plant?
Not necessarily. A 120 TPH plant has 50% higher rated production capacity, but its purchase price does not automatically increase by the same percentage. Actual cost differences depend on the equipment configuration, component specifications, automation, environmental systems, and auxiliary facilities.
How Much Asphalt Can A 120 TPH Plant Produce In A Day?
At its rated capacity, a 120 TPH plant can theoretically produce 960 tons during an 8-hour shift. At 75% operating efficiency, estimated output would be approximately 720 tons. Actual daily production depends on material moisture, mix design, operating hours, maintenance, and transportation arrangements.
Can An 80 TPH Asphalt Plant Handle Highway Construction Projects?
Yes. An 80 TPH plant can handle many highway construction projects, especially when daily asphalt demand is moderate and the project schedule allows sufficient production time. Contractors should compare the required daily tonnage with actual plant output before selecting equipment.
Does A 120 TPH Asphalt Plant Consume More Fuel?
Generally, a 120 TPH plant consumes more fuel per operating hour when producing at a higher output. However, fuel consumption per ton may be similar or lower if the larger plant operates efficiently. Buyers should compare actual liters of fuel per ton under equivalent aggregate and mix conditions.
How Many Trucks Are Needed For A 120 TPH Asphalt Plant?
The required number depends on truck payload, transportation distance, loading time, unloading time, and paving speed. For example, with 20-ton trucks and a 60-minute round trip, approximately six trucks would be needed to transport 120 tons per hour continuously, assuming no additional delays. Longer distances or slower loading and unloading operations require more vehicles.
Can I Upgrade From An 80 TPH Plant To A 120 TPH Plant Later?
Upgrading depends on the original plant design and the capacity limits of its major components. Some auxiliary systems may allow expansion, but the drying drum, burner, screening system, mixer, dust collector, and control system may require substantial modifications or replacement. If future expansion is likely, discuss this requirement with the manufacturer before purchasing the initial plant.
10. Get The Right Asphalt Plant Capacity For Your Construction Business
So, is a 120 TPH asphalt plant worth the additional cost compared with an 80 TPH model? The answer depends on how much asphalt your business can realistically produce, transport, and sell.
If your projects require high daily output, your equipment fleet can support continuous production, and the additional tonnage can generate sufficient returns, a 120 TPH asphalt plant may be a more profitable long-term investment. However, if your demand remains moderate or seasonal, an 80 TPH plant may provide better capital efficiency and lower investment risk.